Skip to content
Home / Capabilities / Box Build

FINISHED-PRODUCT ASSEMBLY AND TEST CAPABILITIES

Box Build Assembly & Testing Capabilities

EBest PCBA provides box build assembly, including PCBA integration, enclosure assembly, cable harness installation, firmware programming, functional testing, and final packaging.

Engineering response target: within 24 hours after receiving your project details.
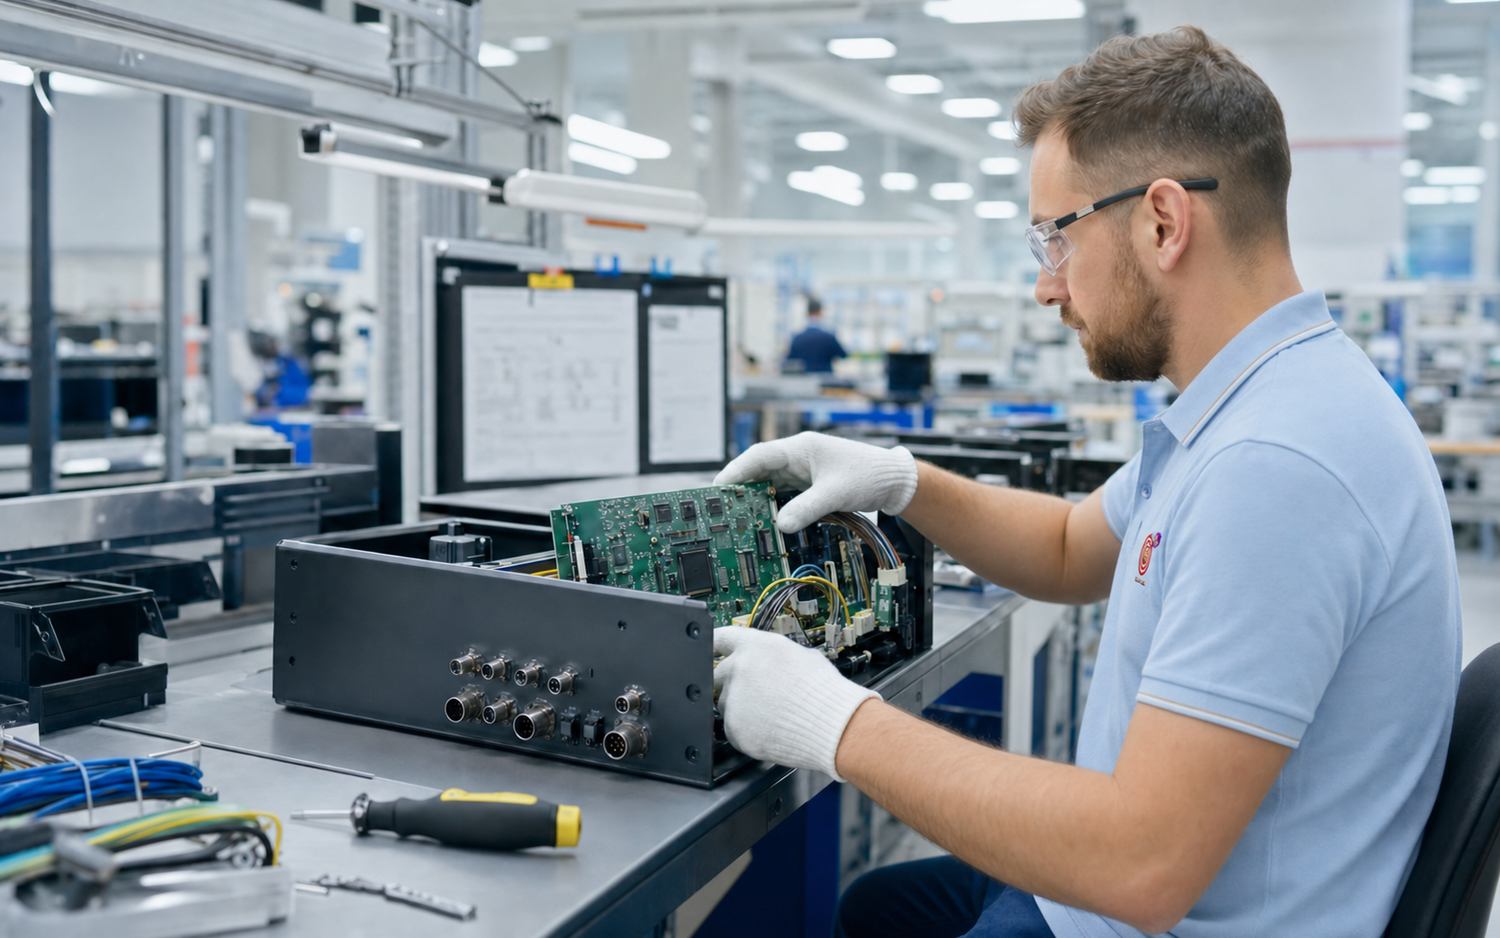
Box-Build Integration Engineer integrating a PCBA and cable harness into an industrial electronic enclosure
Box-build integration from mechanical assembly through final inspection.
One Partner for Complete AssemblyBring PCBAs, enclosures, cables and testing together with one manufacturing partner.
From Prototype to ProductionGet assembly support for your first build and the production orders that follow.
Tested to Your RequirementsProduct-specific functional testing helps verify your finished units before shipment.
Traceability for Repeat OrdersConnect materials, firmware and test records to support consistent repeat builds.

Capability and acceptance matrix

Box Build Manufacturing Capabilities

Manufacturing CapabilitySpecificationsQuality Control
Enclosure integrationUp to 1 × 1 m product formatCAD, weight, access, tolerance, work sequence and safe handling
Cable & harnessRouting, connector insertion, labeling, fastening and continuity checksDrawings, pin map, bend radius, pull/retention criteria and supply responsibility
Fastening & mechanicsScrews, brackets, heat sinks, gaskets, adhesives and thread-locking processesTorque values, tool control, cure conditions, sequence and cosmetic criteria
Conformal coatingUp to 700 × 400 mmMaterial, keep-out zones, coverage, thickness, cure and inspection method
Router depanelingUp to 800 × 400 mmPanel structure, thickness, support, stress-sensitive parts and edge criteria
Programming & configurationFirmware, bootloader, parameter loading, calibration and version verificationFirmware programming, calibration, configuration checks, and revision verification.
ICT / FCTBoard-level checks and custom finished-unit functional fixturesTest access, software, limits, fixture responsibility, maintenance and failure route
Cleanroom route100 m² ISO 7 (Class 10,000) cleanroom route, subject to process reviewApplicable assembly stage, cleanliness standard, clothing and handling requirements
SerializationLaser-marked 2D code and MES-linked unit identityCode format, data ownership, scan points and customer data interface
Final releaseFour-stage final inspection covering functional, mechanical, cosmetic, and packaging checksFunctional, mechanical, cosmetic, label, accessory and packaging criteria

Controlled integration route

Box Build Assembly Process

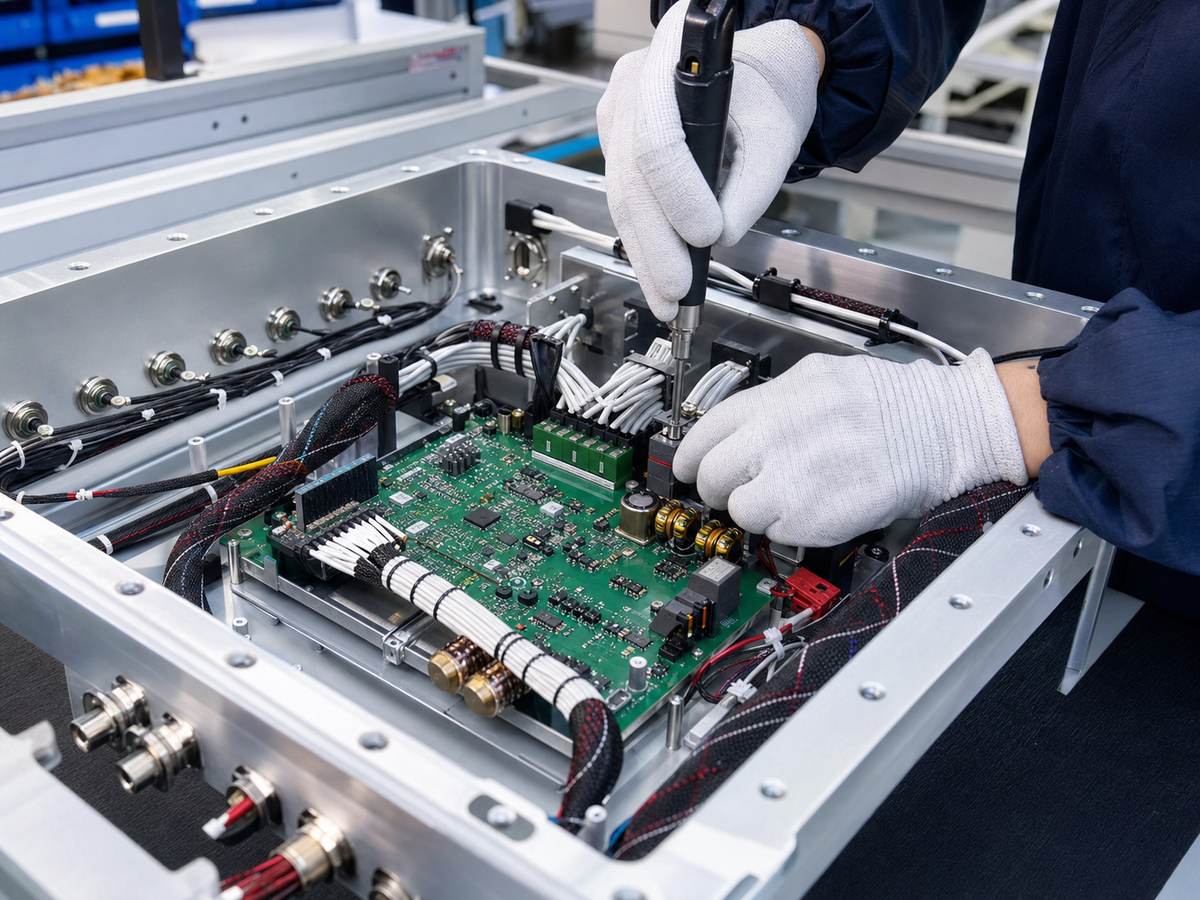
Cable harness routing and controlled fastening inside an electronic enclosure
Product assembly workflow from incoming parts through completed unit.
01

Engineering & Production Preparation

Review BOM, drawings, harness data, firmware, test limits, labels, packaging and volumes.

02

Incoming Material and Subassembly Inspection

Confirm supplied parts, enclosure condition, cable identity and controlled subassemblies.

03

Mechanical Integration

Integrate PCBAs, wire harnesses, heat sinks, fasteners, and mechanical components into the enclosure.

04

Firmware & Configuration

Load the approved revision, verify identity and record configuration where required.

05

Test & Inspection

Run agreed unit-level functions and inspect mechanics, labels, accessories and cosmetics.

06

Final Inspection & Packaging

Link the unit record, complete final inspection and release the approved pack-out route.

Test and release evidence

PCBA Inspection and Finished-Unit Testing

EBest PCBA supports SPI/AOI/X-ray inspection and functional testing, including product-specific test fixtures and recorded test results.
Board-level controlAOI, X-ray, ICT, flying probe or PCBA functional checks are selected from board risk and test access.
Finished-unit FCTFunctional testing can cover power-up, communication interfaces, sensors, loads and indicators, according to your product requirements.
Fixture controlProduct-specific test fixtures support repeatable functional verification, with controlled calibration and maintenance.
Failure & retestFailure codes, isolation, rework authority, retest rules and final disposition are part of the approved test route.
Final inspectionMechanical fit, cosmetics, labels, accessories, packaging and shipment release are checked independently of electrical pass status.

Review testing & inspection equipment →

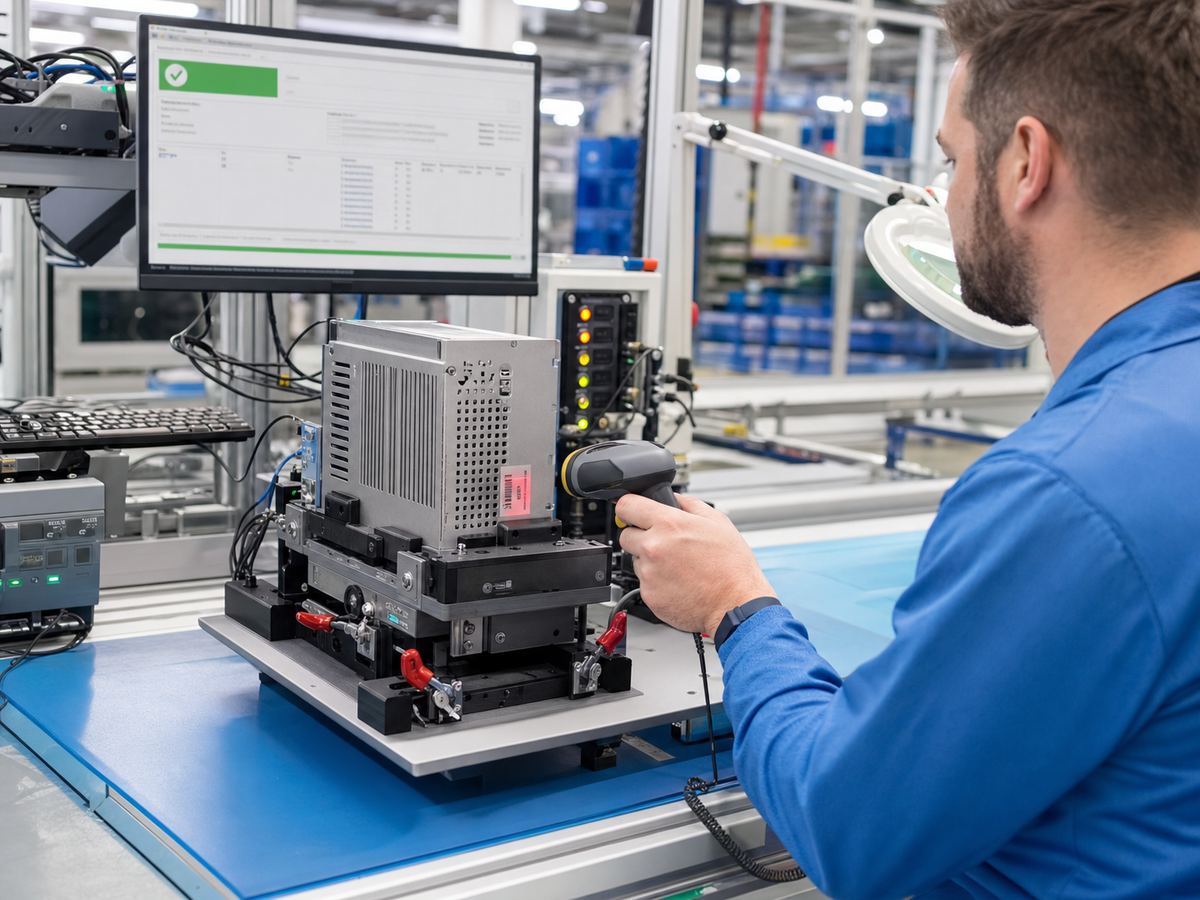
Finished electronic unit connected to a functional test fixture and serial verification station
Finished-unit functional testing with product-specific fixtures and software.

Unit-level traceability

MES Traceability – From Materials to Shipment

For projects using MES traceability, each finished unit can be linked by a laser-marked 2D code to materials, firmware revisions, test results, inspection, and shipment records.

01Unit ID

2D code or customer serial rule

02Materials

PCBA lot, harness and controlled parts

03Configuration

Firmware, bootloader and parameters

04Test Result

Limits, pass/fail and retest status

05Inspection

Mechanical, label and cosmetic release

06Shipment

Pack-out and final release status

Box-build project requirements

Box Build Applications & Project Types

Profile 01

Industrial Controller Integration

Assembly Requirements
Enclosure, harness, I/O map, firmware and functional limits
Manufacturing Considerations
Connector routing, thermal contact, configuration and interface test
Testing & Inspection
Unit ID, firmware revision, FCT and final inspection status
Profile 02

Controlled Cleanroom Assembly

Assembly Requirements
Cleanliness requirements, sealed parts, labels and pack-out criteria
Manufacturing Considerations
Applicable ISO 7 stages, handling, contamination and visual acceptance
Testing & Inspection
Released work route, inspection and traceability records as agreed
Profile 03

Large-Format Electronic Enclosure

Assembly Requirements
Full CAD package, weight, lifting notes, cable drawings and packaging plan
Manufacturing Considerations
Published 1 × 1 m format, work sequence, access and transport protection
Testing & Inspection
Released assembly route, final inspection and shipment status

Quote-ready package

Request a Box Build Assembly Quote

Send your BOM, mechanical drawings, target quantities, and available assembly requirements. Our engineering team will review your project and advise on the next steps.

Request a Box Build Quote
  • BOM and approved component requirements
  • PCBA manufacturing data and drawings
  • Mechanical CAD, enclosure and assembly drawings
  • Cable, harness, connector and pin-map files
  • Torque, adhesive and thermal-interface requirements
  • Firmware, configuration and calibration files
  • Functional test limits or golden sample
  • Labels, serial rules and traceability requirements
  • Packaging, accessories and cosmetic criteria
  • Prototype quantity and production forecast
01

First Response

Target within 24 hours: confirm receipt, NDA status and missing information.

02

Capability Review

Review product dimensions, component supply, assembly methods, test fixtures, and acceptance requirements.

03

Quotation Baseline

Confirm scope, schedule, fixtures, evidence, revisions and commercial responsibilities.

04

NPI & Release

Turn the approved package into pilot instructions, validation and repeatable production.

Discuss Your Box Build Project With Our Engineers

Send your BOM, assembly drawings, test requirements, and target quantities to sales@ebestpcba.com. Our engineers will review manufacturability, assembly scope, and quotation details.

Box build capability FAQ

Box Build Assembly FAQs

What should I send for a box build capability review?
Send the available BOM, PCBA data, mechanical drawings, cable or harness drawings, firmware requirements, test criteria, labeling, packaging requirements and target quantities. EBest PCBA can identify missing inputs during the first review.
Can EBest PCBA link firmware versions and unit-level test results to each serial number?
Yes, when this traceability is included in the approved production process. Firmware, configuration, calibration, functional-test and final-inspection records can then be linked to a unit identifier.
Does EBest PCBA support functional test fixtures?
Yes. Fixture development and functional testing can be included after test access, limits, software, ownership, maintenance and release evidence are confirmed during quotation.
Can EBest PCBA provide cleanroom box build assembly?
Yes, for supported programs subject to process review. Published capability includes a 100 m² ISO 7 (Class 10,000) cleanroom route; product requirements and the applicable assembly stage are confirmed from the project files.
How are box build revisions controlled?
The approved BOM, drawings, firmware, work instructions, test limits and packaging requirements form the released baseline. Changes are reviewed for scope, schedule and cost before revised work proceeds.
Can I request an NDA before sending files?
Yes. Request the NDA first, then send controlled drawings, BOMs, firmware notes or test requirements through the agreed communication route.
Request a Quote